
Product Advantages:
Stable air supply
Reduced pulsation
Peak demand capacity
Condensate removal
Certified safe design
Model | FA-1000 | FA-600 | FA-1100 |
Job Title
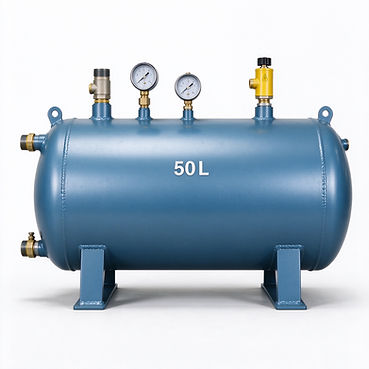
Air Receiver Tank 50L
Model:
FA-1000
Compressed air receiver tank with a 50-litre capacity for storing compressed air and stabilising system pressure in pneumatic installations. It smooths pressure pulsation, provides reserve capacity for peak demand and helps remove condensate, improving overall system efficiency, making it an essential component for reliable plant air supply.
Key Features:
50 litre storage capacity
Stabilises system pressure
Smooths pressure pulsation
Condensate drainage point
ASME / PED certified design
Reliable welded construction
Technical Data:
Capacity: 50 L
Working pressure: up to 11 bar
Media: compressed air
Temperature range: -10 to +80 °C
Connections: G1/2 in/out
Drain: manual / automatic
Certification: ASME / PED
Material & Specifications:
Shell: carbon steel
Coating: epoxy / paint
Feet: steel
Drain valve: brass
Safety valve: brass
Applications:
Compressor air storage
Pressure stabilisation
Peak demand supply
Plant air networks
Condensate separation